Control system migration and upgrade to TIA Portal
Is your stacker crane or conveyor system still running on a Simatic S5, an S7-300, an S7-400 or an S7-mEC? Then your installation depends on a control system whose spare parts are running out. We move it to Siemens Simatic S7-1500 and TIA Portal, without you having to replace the installation.
That can be a full migration, but it can also be a small upgrade: the PLC and the software only, leaving the rest of the installation untouched.
We work from our own software framework for stacker cranes and conveyor systems, running on Siemens Simatic S7-1500F.
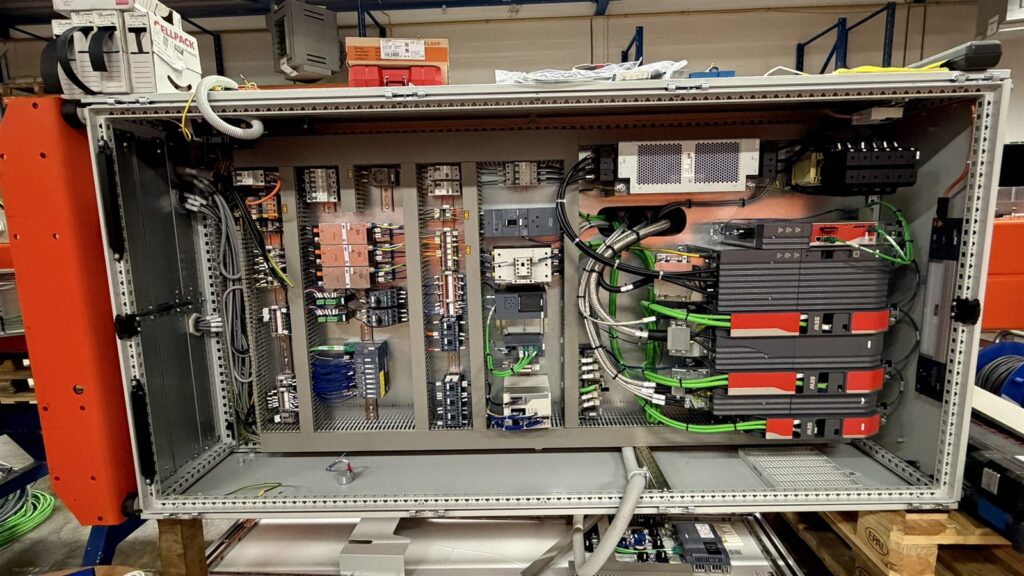
From Simatic S5 to S7-1500
Have you done this before?
Yes. A large share of the retrofits we have carried out came from exactly this: a control system that could no longer be maintained, while the installation itself was still perfectly sound.
So anyone calling us about an obsolete control system is calling about the work we do most often.
Why does a Simatic S5 have to be replaced eventually?
Because Siemens took the S5 out of production decades ago. New parts are no longer made; what is still available comes from remaining stock and from dismantled installations.
As long as everything runs, you notice none of this. That changes on the day a central unit or an I/O card fails. You are then dependent on whatever can be found at that moment, at whatever price is asked for it.
My S5 has run for thirty years without trouble. Why act now?
Understandable. But an S5 that has run for thirty years proves that the installation was well built, not that spare parts exist.
The difference lies in who chooses the moment. Migrate while the installation is running and you plan the downtime yourself. Wait until something breaks and the moment is chosen for you, usually the worst possible one.
There is more to it: who can still work on it? Every year there are fewer engineers who can read STEP 5 and fix an S5 fault.
Is the existing program converted or rewritten?
Neither. We do not start from scratch, and we do not convert blindly either.
For stacker cranes and conveyor systems we have our own software framework that already contains the recurring functionality: positioning, motion profiles, load handling, transport routing, diagnostics and alarm handling. It runs on Siemens Simatic S7-1500F.
What remains is the part specific to your installation. That shortens the lead time considerably and it limits the risk: most of the software has already proven itself elsewhere.
There is another reason. An S5 program that has grown over thirty years contains ways of working that stem from the constraints of that time. Carrying those over one to one means taking those constraints into a control system that no longer has them. We work out what the installation has to do, and build that up with our framework.
Does the whole control cabinet have to be replaced?
Usually yes. That is a deliberate choice, not additional work.
Time on site becomes shorter. A new cabinet is built and tested beforehand at our own workshop. What remains at your site is connecting and commissioning. Rebuilding the existing cabinet means all of that work happens on your premises, during the hours your installation is down.
The result is more reliable. Leaving obsolete components in an otherwise renewed installation means keeping the weakest link. The first fault then comes from exactly that part, just after the installation has been handed over.
How much downtime does a migration cost?
That depends heavily on the scope of the migration, and the difference is large enough to make a decision about it beforehand.
Replacing only the control system is considerably faster: the existing cabinet and wiring stay in place, and the work on site is limited to swapping, connecting and testing.
Replacing control system and cabinet takes more time on site, because the field wiring is laid again as well. In return you are set for years, and we build and test the cabinet beforehand at our own workshop.
Which of the two makes sense for you depends on the condition of the existing installation. We assess that on site and set out both sides, including what each means for your downtime. That way you can make the trade-off yourself.
What does it deliver, apart from being supported again?
Diagnostics that tell you what is wrong instead of that something is wrong. Remote support, so that a fault is often resolved before anyone is on the road. Components that stay available for years. And documentation your own maintenance department can read.
Does this apply to S7-300 and S7-400 as well?
For the S7-300 it is no longer a question: it has been discontinued.
Siemens announced the phase-out of the S7-300 and ET 200M on 1 October 2023 and ended delivery as a new product on 1 October 2025. Since then the components are available only as spare parts or through repair, in limited quantities. What is left is getting scarcer and more expensive.
The S7-400 is on the same path, only later. If your installation runs on one, you still have time. Even so, planning the step is wiser than waiting for it.
If an extension or a rebuild is on your agenda anyway, this is the moment to move to S7-1500 and TIA Portal along with it.
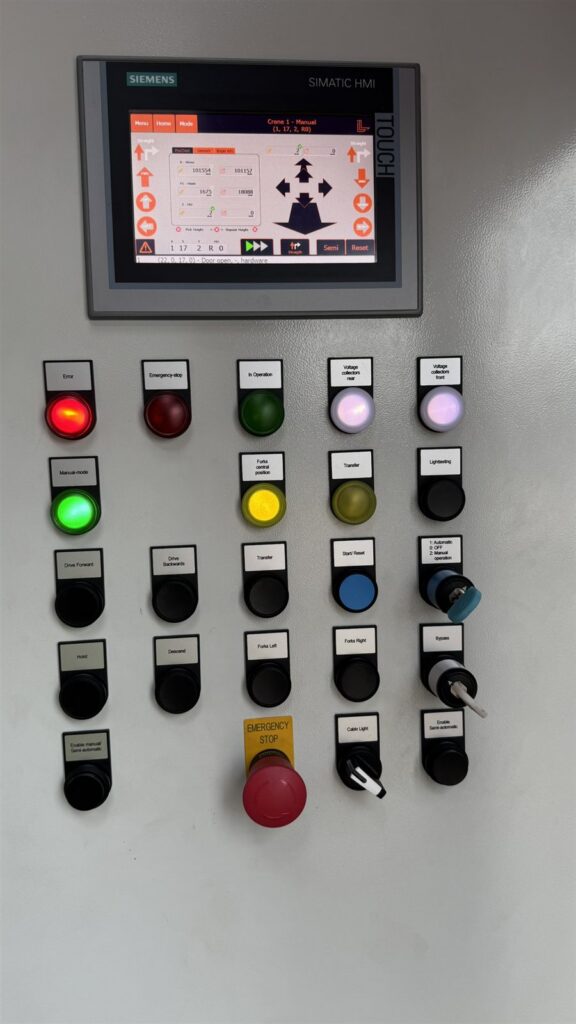
Siemens S7-mEC that is no longer available
My installation runs on an S7-mEC. Why is that a problem?
Because the product is no longer supplied. If the unit fails, there is no equivalent replacement to order. You then depend on whatever the second-hand market happens to offer that day.
The S7-mEC sits in the S7-300 form factor, and that whole family has been discontinued. So it is not just that one controller you are missing. The rack, the power supply and the I/O cards around it have also been unavailable as new since 1 October 2025. Every part has to come from the second-hand market.
With an embedded controller there is something further on top of that. The control system does not run on a classic PLC but as software on hardware with a lifecycle of its own. If that hardware disappears, you lose not only the control system but the platform underneath it.
This controller was widely applied in warehouse systems at the time, including installations by Lalesse. If you have such a unit, this question will come up before long.
What can an S7-mEC be replaced with?
With a Simatic S7-1500 as a hardware PLC.
That is the platform we standardise on and the one our software framework for stacker cranes and conveyor systems runs on. Components stay available for years, and it is a control system for which engineers can be found anywhere, including if you ever want to continue with another party.
The step back from a software-based control system to a real PLC is deliberate. You get a control system that stands on its own, instead of software that depends on the lifecycle of the computer underneath it.
Will my operation and visualisation keep working?
Your higher-level system is left untouched; the operator panels are renewed.
The warehouse control system you work with stays the same. Your processes, your order flows and the way your people run the warehouse therefore do not change.
The HMI panels at the installation we do replace. They belong to the old control system and come along in the migration. Your operators get panels that respond faster and that, in the event of a fault, show what is wrong instead of only that something is wrong.
What happens to the existing I/O and field devices?
The control cabinet can usually stay in place for this migration. That is the big difference from an S5 migration.
An installation with an S7-mEC is considerably younger than one with an S5. The cabinet, the field wiring and the I/O are generally still sound. We replace the control system and the HMI panels; the rest stays as it is. That saves a great deal of downtime and cost.
We do advise going through the cabinet at that moment for components that have themselves been phased out. Whatever is already unavailable is best dealt with straight away: the cabinet is open anyway, and this is the cheapest opportunity you will get.
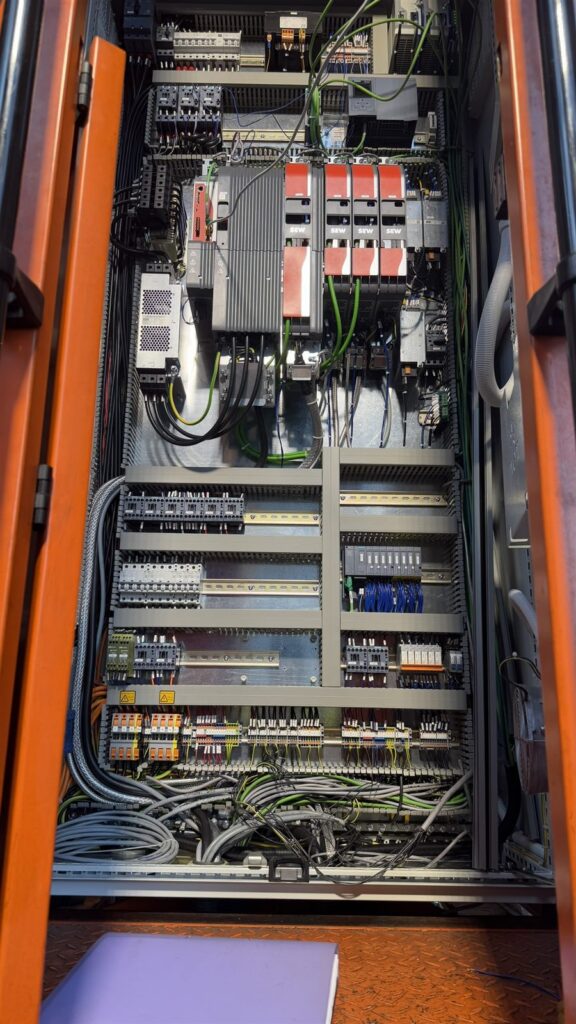
Small upgrade: from STEP 7 to TIA Portal
What does a small upgrade involve?
Hardware and software, but only the control part.
The PLC comes out and a Simatic S7-1500 goes in. We move the program to TIA Portal: the engineering environment Siemens supports and for which people can be found anywhere.
The rest of your installation stays as it is: the control cabinet, the field wiring, the I/O and the mechanics. That is the difference from a full retrofit, and it saves considerably on downtime and on cost.
Why TIA Portal and not STEP 7?
Because STEP 7 Classic belongs to a generation that is being phased out. TIA Portal is where Siemens puts its development, and it is what an engineer leaving college today has been taught.
More practically: with a project in TIA Portal you no longer depend on someone keeping an old programming environment alive on a computer nobody dares to replace.
When is a small upgrade enough, and when is it not?
A small upgrade is enough when the cabinet, the wiring and the field devices are still sound and the control system is the only problem. That is typical of an installation running on an S7-300 or an S7-mEC that has otherwise been properly maintained.
If the cabinet itself has aged, the drives are due for replacement, or parts are running out there as well, a full retrofit serves you better. If the small step will not get you far enough, we will tell you.
Is your installation still running on an obsolete control system?
Tell us which make you have, what year it was built and which control system is in it. We will tell you what is possible, and whether it can wait.